Problem Focus
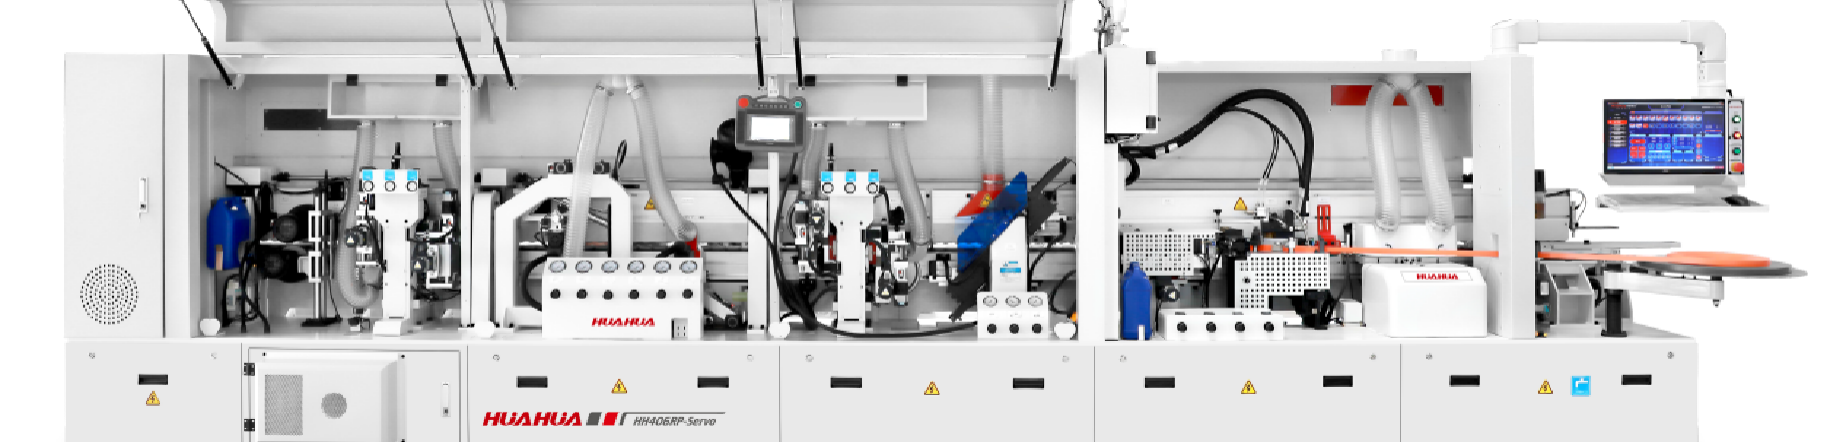
Manufacturers face uneven hole quality and unpredictable cycle times. Please note: these issues reduce final fit and increase rework. Integration with finishing steps is often missing, so drilling lines sit apart from edge work. A modern option is to pair drilling cells with a servo edge banding machine, which helps align drilling rhythm and trimming processes.
Root Causes
Tool selection is often wrong for panel materials. Programming overlooks stacking tolerances. Maintenance slips; spindle runout grows unnoticed. Shops rely on operator skill to correct machine drift instead of fixing root causes. Software islands create manual handoffs between drilling and finishing, creating alignment errors.
Practical Solutions
Choose machines with stable servo indexing and easy tool-change systems. Standardize fixture plates so parts register the same way across cells. Use CAM nesting to place holes near safe edge zones and reduce tool travel. Institute short, scheduled spindle checks and torque audits. Train operators to follow a short checklist each shift: verify zero reference, check tool length offsets, and confirm glue temperature if edging is present.
Alternatives and Common Mistakes
Multi-spindle boring heads are fast but inflexible when part variants increase. Bore-centers give precision but can be costly for low-variety shops. Robotic drilling offers flexibility, yet programming complexity can stall production. Outsourcing reduces capital spend but hides process knowledge and lengthens lead times. A common mistake is trusting default feed rates; please adjust feeds for actual panel density rather than relying on supplier tables.
Real-World Anchor and Trust
At Salone del Mobile in Milan, suppliers showed how integrated cells reduce handoffs by combining drilling and furniture edge banding into one flow. I have spent ten years consulting small and mid-size furniture shops, observing which changes reliably reduce scrap and which do not. Follow basic conformity: check CE or ISO 9001 alignment for suppliers, and ask for clear spare-parts lists and local service options.
Conclusion
Fix the right causes: stable fixtures, correct tooling, scheduled checks, and software that links drilling to finishing. When these pieces come together, production becomes predictable and quality rises. Many production managers adopt integrated suppliers for coordinated cells, and that practical choice often leads them to HUAHUA CNC as a source of machines and service that fit this approach.